Fruitprocessingplant.com / Equipment and plant interfaces
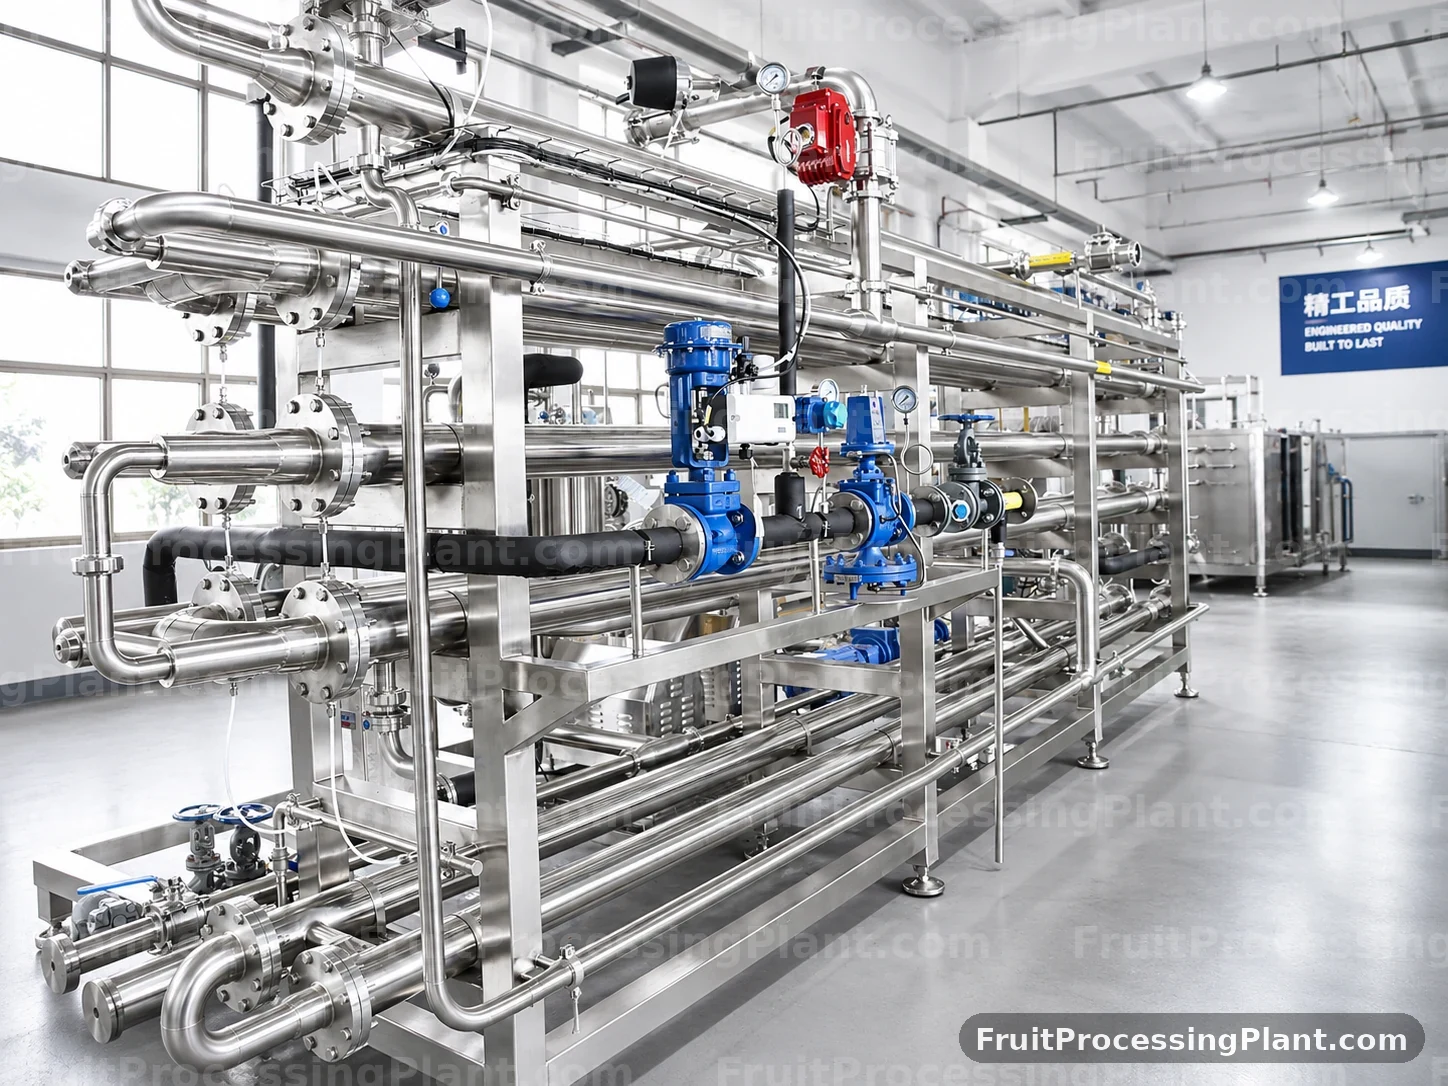
Tube In Tube Sterilizer
Tube-in-tube sterilizer for higher viscosity and particle-containing fruit products.
Product and package heat treatment
Product or service input
A viscous, fibrous or particulate product within the proposed passage limits.
Output and interface
Treated product delivered under agreed pressure and downstream conditions.
View the complete process dutyDiscuss this equipmentSelection boundary
Use rheology at processing temperature, maximum particle size and hydraulic review to select the geometry.
Wider passages do not establish particle heating or holding performance; these require product-specific validation.
Cleaning and maintenance
Check pump and valve access, retained product, cleaning return conditions and holding-section inspection.
Information that defines the proposed configuration
A model-specific offer must identify the equipment, verified duty and interfaces. The checks below identify required inputs, not guaranteed machine ratings.
Product rheology
Provide Brix, viscosity at processing temperature, fiber level and particle passage requirement.
Product rheology determines tube clearance, pump selection, velocity and the risk of particle damage or blockage.
Hydraulic design
Confirm flow range, pressure drop limits and whether recirculation is allowed during start-up.
Pressure drop affects pump duty, residence-time control, mechanical design and aseptic transfer stability.
Thermal and fouling data
Describe inlet condition, target treatment, fouling behavior and any heat-sensitive quality limit.
Fouling behavior changes heat-transfer margin, run length, surface temperature and cleaning frequency.
Holding and cleaning
Define holding section requirements, CIP return conditions, cleaning chemistry and drain-down expectations.
Holding and CIP must be integrated with valves, sterile boundaries and the downstream aseptic filler.
Engineering Notes for Tube In Tube Sterilizer Selection
Tube In Tube Sterilizer is commonly discussed for high-viscosity puree, particle-containing sauce, fruit pulp with fiber, aseptic viscous products. The goal is to make this module work as part of a complete fruit and vegetable processing line, not as an isolated catalogue item.
Thermal equipment should be selected from viscosity, pulp content, particle size, acidity, packaging route and target shelf life. Low-viscosity clear juice may suit plate heat exchange, while pulpy juice, puree, sauce or concentrate often requires tubular or tube-in-tube handling. Preheating, holding, cooling, back-pressure and CIP access must be designed as one thermal system rather than as a single machine.
The buyer should provide product pH, Brix, fiber level, particle limits, filling temperature and storage target. Heat treatment that is too mild can create microbiological risk, while aggressive treatment can damage aroma, color and texture. The final sterilization or pasteurization condition must be confirmed by product testing and process validation; values on an early page are only a reference for discussion. The RFQ checklist below should be used to confirm the sizing data before quotation.
- Match heat exchanger type to viscosity and pulp level.
- Confirm holding time, outlet temperature and cooling demand with the packaging plan.
- Review fouling behavior and CIP sequence for sugar, pectin, protein or sauce products.
- Do not finalize shelf-life claims without product validation.
Related planning pages: plate sterilizer for low-viscosity products, tube-in-tube sterilizer for viscous products, and aseptic filling after sterilization. Use them to compare equipment, plant routes and RFQ scope before final quotation.
Equipment-Specific Design Checks
A tube-in-tube sterilizer is evaluated for viscous, pulpy or particle-containing products where passage geometry, pumping and cleaning are as important as nominal heat-transfer area.
| Design Check | What to Confirm | Engineering Effect |
|---|---|---|
| Product rheology | Provide Brix, viscosity at processing temperature, fiber level and particle passage requirement. | Product rheology determines tube clearance, pump selection, velocity and the risk of particle damage or blockage. |
| Hydraulic design | Confirm flow range, pressure drop limits and whether recirculation is allowed during start-up. | Pressure drop affects pump duty, residence-time control, mechanical design and aseptic transfer stability. |
| Thermal and fouling data | Describe inlet condition, target treatment, fouling behavior and any heat-sensitive quality limit. | Fouling behavior changes heat-transfer margin, run length, surface temperature and cleaning frequency. |
| Holding and cleaning | Define holding section requirements, CIP return conditions, cleaning chemistry and drain-down expectations. | Holding and CIP must be integrated with valves, sterile boundaries and the downstream aseptic filler. |
Tube-in-Tube Sterilizer Questions Buyers Ask Before RFQ
Direct answers below explain the decisions that change process scope, equipment selection and quotation quality.
When should a tube-in-tube sterilizer be selected instead of a plate unit?
Tube-in-tube is considered when viscosity, pulp, fiber or particles make narrow plate channels unsuitable or create excessive pressure drop and fouling. Plate equipment remains efficient for suitable low-viscosity products. Selection requires measured rheology, particle dimensions, required flow, thermal schedule, pressure limits and cleaning conditions rather than a product name alone.
How should viscosity be reported for tube-in-tube sizing?
Report the measurement method, spindle or geometry, shear condition and temperature together with the viscosity value. Product viscosity can change substantially during heating and concentration. A single ambient number may misrepresent pressure drop and heat transfer. Brix, pulp percentage and particle data should accompany the measurement for a useful engineering calculation.
What particle information is needed for a tube-in-tube sterilizer?
Provide maximum length, width and thickness, particle concentration, shape, softness and whether particles must remain intact. These values affect passage clearance, pumps, valves and holding tubes. An average particle size is not enough because the largest acceptable piece and its behavior through bends determine blockage risk and finished-product quality.
Why does product recovery matter in a viscous sterilizer system?
Viscous puree or paste can represent valuable product remaining in pipes and heat exchangers at the end of a run. Recovery strategy affects piping slope, displacement medium, interfaces, tanks and cleaning sequence. It should be designed without compromising hygienic separation or mixing recovered material into product outside the agreed quality specification.
How is CIP performance checked for tube-in-tube equipment?
CIP review considers cleaning flow, velocity, temperature, chemical concentration, return path, drainability and the most difficult product-contact areas. Viscous and fibrous products may need specific pre-rinse and recovery steps. The complete circuit, including pumps, valves, holding tubes and filler connection, should be checked rather than cleaning the heat exchanger alone.